Table of Contents
Heavy duty pipe cutting machine: Evaluate support and clamping together so holding force does not create ovality or movement. For clamping large diameter pipe, the review should connect support position, clamp force, and ovality. The purpose is to establish what must be checked before the next production or purchasing decision, using the finished-part drawing and representative stock conditions as the controlling reference.
When assessing a heavy duty pipe cutting machine, use the finished-part drawing and representative stock conditions for the project-specific limits and inspection method. The following checks connect support position with clamp force and ovality.
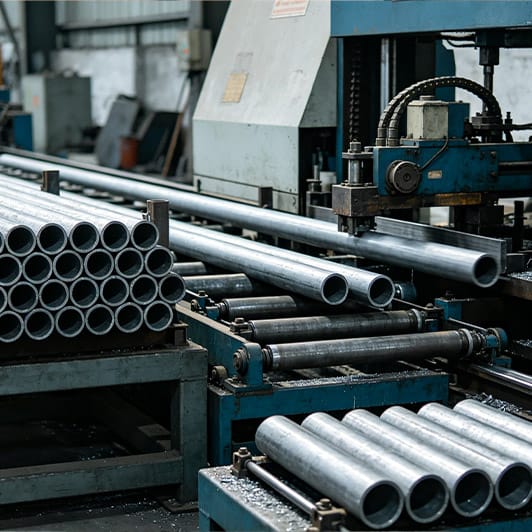
1. Support position: the first check
In a heavy duty pipe cutting machine project, for clamping large diameter pipe, compare support position with clamp force and ovality under the same identified configuration. Evaluate support and clamping together so holding force does not create ovality or movement.
For buyers reviewing a heavy duty pipe cutting machine, the clamp must hold the pipe consistently without creating unacceptable distortion. Review support positions and contact areas with the supplier. Observe movement during representative cuts and measure the released part. Increasing force can reduce slip while worsening ovality, so workholding should be evaluated as a balanced arrangement.
In a heavy duty pipe cutting machine project, for larger sections, inspect the pipe shape after it is released from workholding. Clamping that prevents movement can also alter a sensitive section. Compare cut geometry with the released shape and discuss the holding arrangement with the supplier. Additional force is not a universal solution to an unstable cut.
2. Clamp force: the connected interface
When assessing a heavy duty pipe cutting machine, cut squareness should be measured relative to the agreed pipe axis. Inspect the face at defined positions and distinguish angular error from a rough or burred edge. Clamping, blade condition, and support behaviour may all influence the result. Recording the pattern is more useful than describing every imperfect end as a blade problem.
In projects involving a heavy duty pipe cutting machine, blade selection depends on the material and section as well as the machine. Confirm the recommended blade type, geometry, and operating conditions with the equipment and blade suppliers. Use representative trials to judge finish, stability, and consumable use. Avoid transferring a successful setup from a very different section without verification.
3. Ovality: the acceptance condition
For buyers reviewing a heavy duty pipe cutting machine, changeovers should identify material, section, recipe, blade, and physical setup. Verify the first accepted cut and record the measurement method. A saved recipe may not capture a different clamp insert or support position. Keep the mechanical setup and control information linked to the same product identity.
For a heavy duty pipe cutting machine, installation planning must include incoming stock length, offcut space, service access, and the surrounding handling route. Confirm the approved machine and foundation layout before site work. A compact machine can still require a long production envelope when processing long pipe. Include that space in capacity planning.
4. Heavy duty pipe cutting machine review options
When assessing a heavy duty pipe cutting machine, the decision table connects clamping large diameter pipe with the evidence needed for support position, clamp force, and ovality.
| Decision point | Evidence to request | What it resolves |
|---|---|---|
| Support position | Defined reference and initial observations | Evaluate support and clamping together so holding force does not create ovality or movement. |
| Clamp force | Installed configuration and connected interfaces | Whether the result changes with setup or handling |
| Ovality | Representative trial and released-product inspection | Whether the agreed acceptance question has been answered |
| Return to routine production | Verified configuration, open actions, and recheck triggers | How the accepted result will be reproduced |

5. Production interfaces for heavy duty pipe cutting machine
In projects involving a heavy duty pipe cutting machine, consumable stock should reflect actual production duty and supplier lead time. Record compatible blade references and the process used to release a replacement into service. Compare accepted cuts and interruption time over representative runs. Avoid turning a short trial into a guaranteed blade-life claim.
For buyers reviewing a heavy duty pipe cutting machine, automatic operation includes loading, discharge, inspection, and recovery after interruption. Review which tasks remain manual and how an operator restarts a partially completed cycle. Count accepted parts across a normal shift condition. A brief cutting demonstration can omit the delays that dominate practical output.
6. A representative verification trial
In a heavy duty pipe cutting machine project, for clamping large diameter pipe, record the incoming or assembled condition, the verified setup or intervention, and the final observation. Identify support position, clamp force, and ovality on the trial sheet. Keep failures and interruptions in the record. If an input, support, or measurement method changes, label the change so the next comparison remains interpretable.
When assessing a heavy duty pipe cutting machine, chip management protects contact and measurement surfaces. Inspect accumulation around clamps, stops, and transfer paths. Follow the supplier’s cleaning and service instructions. Chips left on a locator can create a length or seating error that resembles a control problem, particularly when the error appears intermittently.
Coolant and lubrication arrangements should follow the machine and tooling requirements. Confirm supply, maintenance, collection, and destination-site responsibilities. Include consumables and service access in the quotation comparison. A machine price that excludes the required support arrangement does not describe the installed operating cost.
7. Maintenance and repeatability of heavy duty pipe cutting machine
Transfer datums deserve inspection after chips and burrs are present. A clean empty station may locate correctly while production parts fail to seat consistently. Check the actual incoming condition at the next operation. This connects cutting performance with the facing or chamfering result instead of evaluating two isolated demonstrations.
A changeover trial should include the physical clamp and support changes as well as the selected recipe. Verify the first accepted part and retain its measurements. Similar product names on the controller do not establish identical workholding. The setup record should identify the arrangement actually used for the new material and section.
8. Evidence to include in the technical inquiry
The inquiry for clamping large diameter pipe should include the finished-part drawing and representative stock conditions, the planned material or product range, and observations of support position, clamp force, and ovality. Ask the supplier to identify its proposed configuration, excluded conditions, trial method, and supply boundary. A quotation is easier to compare when it answers these project-specific interfaces.
Explore Huier’s related product information and submit drawings through the technical inquiry page. Keep any proposed change to the requirement separate from a change to the equipment or tooling. Record which party must approve each change before it enters production.
9. Decision checklist for heavy duty pipe cutting machine
Before releasing this project stage, confirm the approved revision, the evidence for support position, the connected check for clamp force, and the acceptance observation for ovality. Identify any product or condition that the trial did not cover. Keep the accepted configuration and the triggers for reinspection together with the order record.
Additional reading: NIST length-unit reference. This reference is provided as technical background, without implying a product certification or an independent assessment of the proposed equipment.
For a heavy duty pipe cutting machine project involving clamping large diameter pipe, send Shandong Huier Heavy Industry the approved drawing, representative input details, and observations for support position, clamp force, and ovality. Request a configuration review and a clearly defined quotation, trial, and inspection scope.
Frequently asked questions
What is the first priority in clamping large diameter pipe?
Evaluate support and clamping together so holding force does not create ovality or movement. Use the finished-part drawing and representative stock conditions to define the acceptance question before changing the setup or ordering parts.
How should support position be recorded for heavy duty pipe cutting machine?
Record the identified configuration and inspection reference. Compare support position with the agreed requirement and retain the connected observation for clamp force.
Why does clamp force matter when reviewing a heavy duty pipe cutting machine?
It is one of the interfaces identified for clamping large diameter pipe. Check clamp force against the project requirement, alongside the evidence for support position and ovality, before assigning a cause.
What trial evidence is needed for heavy duty pipe cutting machine?
Represent the actual input and configuration for clamping large diameter pipe. Retain results for support position, clamp force, and ovality, including failed checks.
What should a supplier proposal for heavy duty pipe cutting machine contain?
It should address clamping large diameter pipe, the defined supply boundary, and the method for verifying support position. Include the finished-part drawing and representative stock conditions in the inquiry.