Table of Contents
Concrete pipe cage welding machine: Verify the finished cage envelope rather than relying only on the nominal machine diameter setting. For cage diameter and cover control, the review should connect cage envelope, wire diameter, and cover spacer. The purpose is to establish what must be checked before the next production or purchasing decision, using the reinforcement drawing and approved inspection requirements as the controlling reference.
When assessing a concrete pipe cage welding machine, use the reinforcement drawing and approved inspection requirements for the project-specific limits and inspection method. The following checks connect cage envelope with wire diameter and cover spacer.
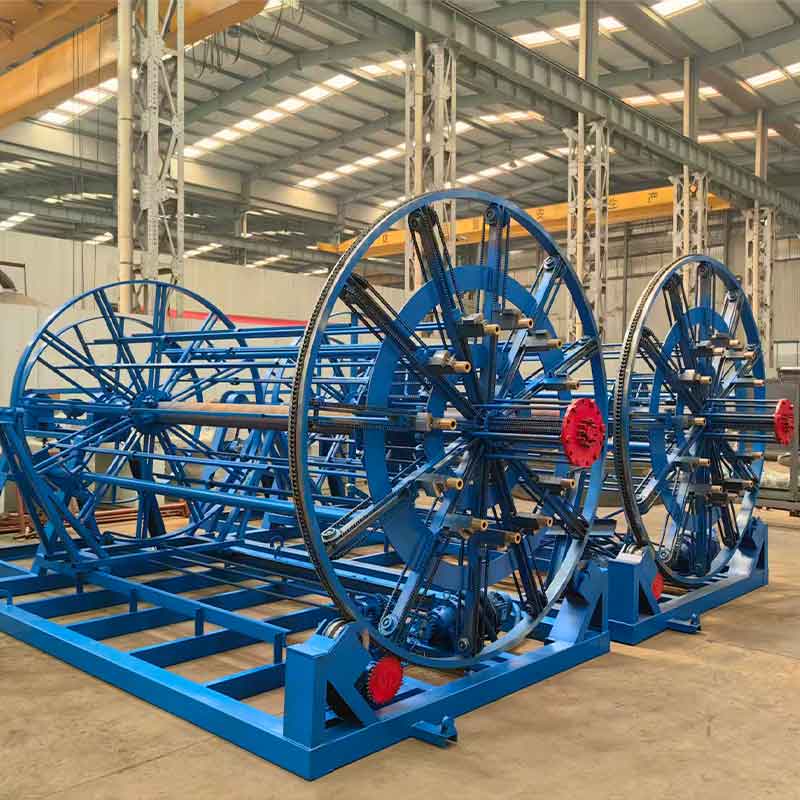
1. Cage envelope: the first check
In a concrete pipe cage welding machine project, for cage diameter and cover control, compare cage envelope with wire diameter and cover spacer under the same identified configuration. Verify the finished cage envelope rather than relying only on the nominal machine diameter setting.
For buyers reviewing a concrete pipe cage welding machine, nominal diameter settings do not replace measurement of the completed cage. Wire diameter, local deformation, and handling can change the envelope that must fit inside a mould. Measure at agreed positions and check ends as well as the central region. The relevant result is a cage that meets the drawing after it is released and handled.
For a concrete pipe cage welding machine, acceptance material should represent the wire specifications proposed for production. A demonstration on one easy configuration may leave uncertainty at another diameter, pitch, or wire arrangement. List untested combinations in the report. That distinction helps purchasing and production teams decide which additional evidence is needed before routine use.
2. Wire diameter: the connected interface
When assessing a concrete pipe cage welding machine, changeovers can involve diameter, pitch, length, wire count, and support positions. Identify every change on a setup sheet. Verify the first completed cage rather than relying only on control-panel values. Keep compatible tooling and instructions together when the line regularly switches among several pipe products.
In projects involving a concrete pipe cage welding machine, plan cage storage supports around the finished dimensions and the transfer into casting. Stacking or unsupported handling can create changes after the welding station has completed its work. Where a dimensional dispute arises, compare measurements before and after the relevant movement. This identifies the stage at which control was lost.
3. Cover spacer: the acceptance condition
For buyers reviewing a concrete pipe cage welding machine, cage cover depends on the relationship between the finished cage and the mould. Review spacers, local wire protrusions, and end positioning during a representative fit check. A cage that meets its overall diameter can still create a local interference. Record the observed location before changing the mould or the welding setup.
For a concrete pipe cage welding machine, service access must match the supplier’s maintenance instructions. Allow room around rotating elements, wire-feed equipment, and control cabinets. Installation drawings should include the paths used for material supply and finished-cage removal. The static machine footprint does not describe the entire workstation.
4. Concrete pipe cage welding machine review options
When assessing a concrete pipe cage welding machine, the decision table connects cage diameter and cover control with the evidence needed for cage envelope, wire diameter, and cover spacer.
| Decision point | Evidence to request | What it resolves |
|---|---|---|
| Cage envelope | Defined reference and initial observations | Verify the finished cage envelope rather than relying only on the nominal machine diameter setting. |
| Wire diameter | Installed configuration and connected interfaces | Whether the result changes with setup or handling |
| Cover spacer | Representative trial and released-product inspection | Whether the agreed acceptance question has been answered |
| Return to routine production | Verified configuration, open actions, and recheck triggers | How the accepted result will be reproduced |
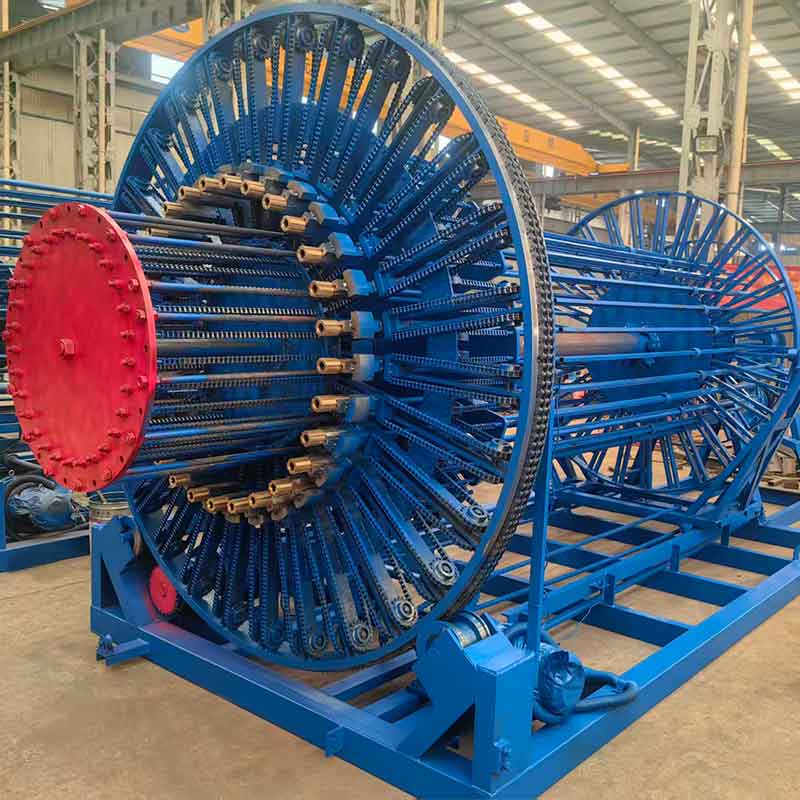
5. Production interfaces for concrete pipe cage welding machine
In projects involving a concrete pipe cage welding machine, support the cage during removal and transport. An accurately welded cage can become distorted if it is carried or stored in an unsuitable arrangement. Plan the transfer into the mould and check clearance before production. Handling is therefore part of dimensional control, even though it occurs after the welding cycle.
For buyers reviewing a concrete pipe cage welding machine, when wire count changes, verify the spacing arrangement and retention of each longitudinal element. A familiar diameter setting can hide a different cage configuration. Check the first completed cage against the reinforcement drawing and record its setup identity. The inspection should confirm the actual cage, not merely the recipe name displayed on the controller.
6. A representative verification trial
In a concrete pipe cage welding machine project, for cage diameter and cover control, record the incoming or assembled condition, the verified setup or intervention, and the final observation. Identify cage envelope, wire diameter, and cover spacer on the trial sheet. Keep failures and interruptions in the record. If an input, support, or measurement method changes, label the change so the next comparison remains interpretable.
When assessing a concrete pipe cage welding machine, compare quotations using the complete cage size and wire specification range. Include feeding, tooling, controls, inspection support, training, and spare parts. Ask the supplier to identify which requirements are standard and which need configuration review. Broad capability language is less useful than a clearly defined supply boundary.
The finished reinforcement cage must satisfy the approved pipe reinforcement drawing. Machine capability does not establish structural suitability. Confirm cage diameter, length, longitudinal wire arrangement, and helical pitch with the responsible design team. Then translate those requirements into setup and inspection points for the welding process.
7. Maintenance and repeatability of concrete pipe cage welding machine
A wire-feed interruption can change the local cage geometry. Mark the affected location and inspect it before deciding whether the product can proceed. Retain the recovery action in the production record. This makes it possible to compare an isolated interruption with a persistent setup problem without assuming they have the same cause.
Helical pitch depends on coordinated feeding and rotation. Measure the finished cage along its length and look for changes near starts, stops, and transitions. A nominal control value does not describe every local result. Investigate repeatable pitch errors by comparing the measured pattern with the process sequence.
8. Evidence to include in the technical inquiry
The inquiry for cage diameter and cover control should include the reinforcement drawing and approved inspection requirements, the planned material or product range, and observations of cage envelope, wire diameter, and cover spacer. Ask the supplier to identify its proposed configuration, excluded conditions, trial method, and supply boundary. A quotation is easier to compare when it answers these project-specific interfaces.
Explore Huier’s related product information and submit drawings through the technical inquiry page. Keep any proposed change to the requirement separate from a change to the equipment or tooling. Record which party must approve each change before it enters production.
9. Decision checklist for concrete pipe cage welding machine
Before releasing this project stage, confirm the approved revision, the evidence for cage envelope, the connected check for wire diameter, and the acceptance observation for cover spacer. Identify any product or condition that the trial did not cover. Keep the accepted configuration and the triggers for reinspection together with the order record.
Additional reading: precast concrete background. This reference is provided as technical background, without implying a product certification or an independent assessment of the proposed equipment.
For a concrete pipe cage welding machine project involving cage diameter and cover control, send Shandong Huier Heavy Industry the approved drawing, representative input details, and observations for cage envelope, wire diameter, and cover spacer. Request a configuration review and a clearly defined quotation, trial, and inspection scope.
Frequently asked questions
What is the first priority in cage diameter and cover control?
Verify the finished cage envelope rather than relying only on the nominal machine diameter setting. Use the reinforcement drawing and approved inspection requirements to define the acceptance question before changing the setup or ordering parts.
How should cage envelope be recorded for concrete pipe cage welding machine?
Record the identified configuration and inspection reference. Compare cage envelope with the agreed requirement and retain the connected observation for wire diameter.
Why does wire diameter matter when reviewing a concrete pipe cage welding machine?
It is one of the interfaces identified for cage diameter and cover control. Check wire diameter against the project requirement, alongside the evidence for cage envelope and cover spacer, before assigning a cause.
What trial evidence is needed for concrete pipe cage welding machine?
Represent the actual input and configuration for cage diameter and cover control. Retain results for cage envelope, wire diameter, and cover spacer, including failed checks.
What should a supplier proposal for concrete pipe cage welding machine contain?
It should address cage diameter and cover control, the defined supply boundary, and the method for verifying cage envelope. Include the reinforcement drawing and approved inspection requirements in the inquiry.